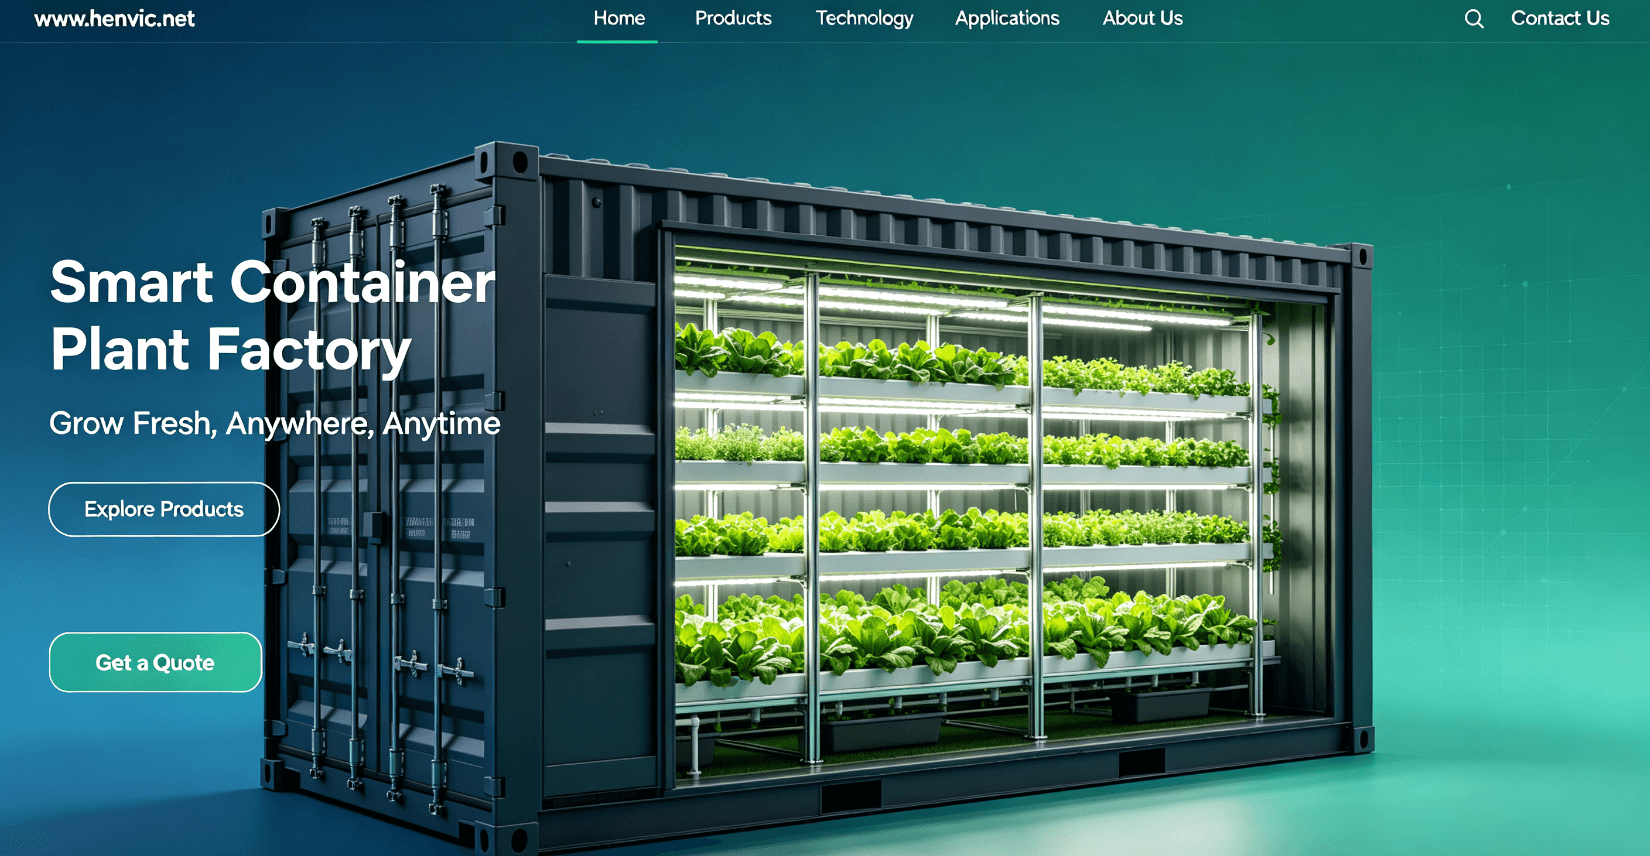
A plant cultivation container is a sealed, thermally isolated, fully instrumented volume in which photosynthesis is the engineered input rather than the ambient condition. That inversion — light supplied as electricity, water supplied as a metered ionic solution, temperature and humidity held against an outdoor environment that is irrelevant to the crop — is what distinguishes the format from a greenhouse and makes it, in engineering terms, a small process plant that happens to grow food. The container's job is not to create favourable weather; it is to make the absence of weather a fixed cost that can be budgeted, and to convert that fixed cost into a production rate that a location without arable land, a working season, or a reliable supply chain can otherwise never obtain.
Understanding the technology requires holding four threads at once: the envelope (what keeps the inside decoupled from the outside), the energy conversion chain (light in, heat and water vapour out), the crop-support systems (root zone, nutrition, CO₂), and the control and reliability layer that determines whether the whole thing is a demonstration or a business.
1. Scope: What Counts as a Cultivation Container
The label covers several distinct products that marketing routinely merges.
- Finishing grow containers — insulated modules with racking, lighting, HVAC and irrigation, used to bring crops to harvest.
- Mobile / modular plant factories — the same idea at higher light density and vertical racking, sold as turnkey units.
- Nursery and propagation pods — running germination (dark, warm, saturated) and hardening-off (low light, high VPD), which is a contradictory climate regime and should not share an air path with a finishing room.
- Hybrid or multi-stage containers — a single shell sequenced through stages. This is almost always a compromise: one air path, one water path and one contamination boundary across functions that want to be separated.
- Specialty enclosures — vessel-mounted, polar-station, mine-camp, disaster-response and garrison units, where procurement is driven by logistics and nutrition rather than cost per kilogram.
The architectural rule that separates serious deployments from showroom units is stage separation: propagation, finishing, post-harvest handling and cleaning are given dedicated spaces and dedicated air, even when they share a power and control backbone.
2. The Envelope: Where the Format Is Won or Lost
The shell is usually a weathering-steel ISO container or a purpose-fabricated panel box, lined internally with cleanable, food-grade surfaces over PU/PIR or rock-wool insulation. Four envelope properties determine everything downstream.
Thermal bridging. A steel frame conducts outside temperature straight into the interior. Without a continuous thermal break, the frame becomes a condensation surface, and condensation in a high-humidity grow room is simultaneously an energy leak, a disease event and a cosmetic defect. Purpose-built panel boxes handle this far more cleanly than a converted box, and the difference shows up in the electricity bill within one season.
Airtightness and pressure discipline. The envelope must be tight enough that incoming air can be filtered and that CO₂ enrichment is not vented to the neighbourhood, but the room also needs a controlled pressure relationship to the outside so that leakage is inward-filtered rather than inward-unfiltered. Light-tightness is part of the same requirement: stray light leaking into a photoperiod-controlled room bolts long-day crops, and light escaping a dark-phase germination room defeats the phase entirely.
Condensation management and drainage. Growing rooms are wet by design. A sloped, trapped, wash-down floor is mandatory; a "sealed floor with no drain" is a specification red flag. Cold bridges, the undersides of light fixtures, and uninsulated refrigerant lines all drip onto canopies, and each drip is a Botrytis or downy-mildew inoculation point plus a grade downgrade.
Structural load. A fully stocked rack of saturated substrate or solution-filled channels is heavy, and a container floor concentrates that load along rack lines. Rack spacing must satisfy two different numbers — airflow between plants and a human body plus a cart working the face — and cheap units optimise the wrong one.
3. Light as the Input: The Dominant Energy Conversion
In the absence of sunlight, electric light is the primary input, and it defines both the productivity ceiling and the thermal load.
Quantities that matter. PPFD (μmol m⁻² s⁻¹, 400–700 nm) sets instantaneous rate; DLI (mol m⁻² day⁻¹) sets cumulative carbon and morphology; uniformity across the canopy plane determines whether one rack yields one grade or three; spectral composition determines form as much as mass. Typical finishing bands for leafy crops sit in the region of roughly 150–300 μmol m⁻² s⁻¹ with DLI targets around 12–17 mol m⁻² day⁻¹, while fruiting crops and high-light herbs push higher and delicate baby-leaf or hardening stages run lower. These are engineering bands, not recipes: genotype, temperature, VPD, CO₂ and nitrogen all move the optimum.
Efficacy and the heat that follows. Modern horticultural LED fixtures commonly deliver around 2.5–3.5 μmol/J at output, with driver losses on top. Nearly all electrical energy fed to the light ultimately becomes heat inside the sealed volume, so a canopy at 250 μmol m⁻² s⁻¹ and 3 μmol/J receives roughly 83 W m⁻² of light power that the cooling system must reject. Lighting is typically the largest electrical load, followed by HVAC.
Thermal management as a process control, not a reliability detail. LED junction temperature drives both lumen depreciation and spectral shift — a hot fixture changes its red-to-blue ratio, which changes crop morphology, which is then misdiagnosed as a seed or nutrient fault. Driver electronics are the most common early failure in a humid environment; their IP rating and mounting location (inside the room versus outside the thermal envelope) should be read on the spec sheet, not assumed.
Spectral programming. Red (≈660 nm) drives photosynthetic efficiency and elongation; blue (≈450 nm) suppresses stem and petiole extension; far-red (≈730 nm) triggers shade-avoidance, lifting leaves out of self-shading and raising harvest index on rosette crops — and, misapplied, bolting long-day species; green penetrates deeper into the canopy and improves visual inspection; UV-B in short low-dose pulses elevates flavonoids and anthocyanins and tightens leaf texture, within a narrow window. A genuine dark period and dawn/dusk ramps improve stomatal behaviour, carbohydrate partitioning and, for bolting-sensitive species, the dark-period temperature and far-red content matter more than total light.
4. The Heat-and-Water Balance: Latent-Dominated by Construction
Inside a sealed pod the energy balance is unforgiving. Sensible gain comes from fixtures, drivers, fans and infiltration; latent gain comes from transpiration, which for a dense canopy is substantial because the water a crop takes up is overwhelmingly lost through stomata. The cooling demand is therefore latent-dominated, and the single most common sizing error in this market is specifying HVAC on cooling capacity alone. A unit sized that way will hit temperature setpoint, cycle the compressor, and let humidity climb until every cold surface weeps.
The correct specification is dehumidification capacity at the design room condition, in litres per day, stated alongside sensible capacity and the assumed canopy density.
VPD is the master variable. Vapour pressure deficit governs transpiration, and therefore governs mineral delivery to leaf margins. Leafy crops are commonly managed in a band of roughly 0.8–1.2 kPa. Run too tight — high humidity, low VPD — and calcium stops reaching leaf tips even when the solution is replete, producing tip burn: a climate-control failure, not a nutrient deficiency, and the most frequent reason a high-yielding pod produces unsaleable product. Run too loose and stomata close, growth stalls, and the crop spends its energy budget on defence instead of leaf area. The mirror consequence is that a crop finished in still, saturated air looks excellent inside the pod and wilts on the shelf, because cuticle and wax development are shaped by VPD and airflow during the finishing phase.
CO₂ enrichment. Ambient air in the low hundreds of ppm is limiting for a well-lit canopy; enrichment to roughly 800–1,200 ppm is standard where economics justify it, delivered as liquid, solid or purified combustion CO₂. It only pays when light, nutrients and temperature are simultaneously non-limiting, and it carries two hazards: a leaky room wastes the gas, and a tightly sealed room accumulates it to a level that is an occupational hazard in an unoccupied space without an interlock. Combustion generators add heat and, if mis-set, nitrogen dioxide — phytotoxic in a sealed volume.
5. Root-Zone Architectures and the Buffer Trade
The delivery system determines labour, contamination risk, and how forgiving the pod is to a control error.
| System | Principle | Strength | Governing risk |
|---|---|---|---|
| NFT | Thin flowing film in shallow channels | Low solution volume, fast response, high oxygen exposure | Catastrophic on pump or power failure; channel clogging; root-zone heating |
| DWC | Roots in aerated solution under a floating raft | High thermal/chemical buffering, robust, simple | Large solution mass slows corrections; anoxia if DO collapses |
| Ebb-and-flow | Periodic flood and drain of a tray | Familiar; good for media and heavy plants | Media adds weight and a pathogen reservoir; drain clogging floods |
| Aeroponic / mist | Droplets sprayed onto suspended roots | Best water/nutrient efficiency, excellent oxygenation, visible roots | Nozzle fouling is the dominant failure; zero buffer volume |
| Media, recirculating | Inert substrate, drip or sub-irrigation | Most forgiving; suits heavy leaf, herbs, fruiting crops | Salt accumulation; Pythium reservoir; disposal logistics |
The underweighted point: solution volume is a buffer, and a buffer is also a lag. A 500 L reservoir drifts slowly and corrects slowly; a 30 L reservoir responds instantly to both a dosing error and a pathogen bloom. The right answer depends on how well dosing and disinfection are engineered, not on a universal preference for large or small.
6. Nutrition Solution Management
This is where container operations quietly lose yield.
Conductivity and pH. Leafy crops commonly run at EC around 1.2–2.2 mS cm⁻¹ depending on species, stage and climate, with pH near 5.5–6.5. pH control and EC dosing are separate loops and must not be conflated: adding acid lowers pH but adds ions that raise EC, and adding base can precipitate phosphate and carbonate salts onto emitters. Acid selection is a formulation decision — phosphoric, nitric, sulphuric and citric acids each shift the ionic balance differently, and citric additionally feeds biofilm.
Dissolved oxygen and temperature. Root respiration needs oxygen, saturation concentration falls as solution warms, and microbial oxygen demand rises at the same time — so warm solution is doubly bad, starving roots and feeding Pythium. Keeping the reservoir cool and well aerated is among the highest-return interventions available, and it is why serious pods place the reservoir outside the hot volume or chill it actively.
Ion drift in a closed loop. Potassium, calcium and magnesium compete for uptake; sodium and chloride accumulate because they are taken up poorly and never leave; nitrate depletion shifts pH. A recirculating system without either periodic exchange or an ion-removal path drifts toward a composition the recipe never specified — the central argument against "zero discharge" as an unqualified virtue.
Disinfection. UV at 254 nm is dose-limited by flow rate, lamp ageing and solution UV transmittance (turbid or iron-rich water destroys the design dose); ozone requires contact time and off-gas destruction; membrane or slow-sand filtration, and in high-throughput practice thermal pasteurisation of the drain-run, are alternatives. Any of these needs a validated dose, not a device that merely exists.
7. Crop-Class Requirements: One Shell, Contradictory Jobs
The container's real technical difficulty is that different crop classes want incompatible environments, and a unit optimised for nothing is mediocre at everything.
- Leafy greens — fast cycles, thin margins, extremely sensitive to VPD (tip burn) and to photoperiod leakage (bolting). The environment must be stable and slightly dry-leaning.
- Fruiting vegetables (tomato, cucumber, pepper) — far higher light and CO₂ demand, longer cycles, and the addition of pollination (vibration, bumblebee or assisted), trellis and canopy load, and a generative-versus-vegetative balance that responds to temperature differential between day and night. Humidity must be managed to prevent grey mould on senescing tissue, and the plant's transpiration is an order of magnitude greater than a lettuce's.
- Strawberries and cane fruit — cold-required dormancy or chilled-runner logistics, high light, narrow EC windows, and extreme sensitivity to crown temperature and to Botrytis on fruit; the highest-value and least forgiving segment.
- Herbs — the highest value per volume and the most sensitive to chilling injury at the reservoir (basil punishes a cold solution) and to airflow that dries leaf edges.
- Microgreens and shoots — very short cycles, low light per crop, high labour intensity, and a strong fit for small-footprint formats and direct channels.
- Medicinal and functional crops — where specific secondary-metabolite targets justify precise spectral and stress manipulation, and where the price per kilogram covers the energy.
- Fungi — a different organism entirely: heterotrophic, no light requirement for colonisation, driven by temperature down-shift and CO₂ drop to trigger pinning, and requiring a warm, high-humidity, low-airflow regime that is the opposite of a leafy room. Fungal production shares the container format but not the light subsystem, and its contamination logic centres on substrate pasteurisation rather than solution hygiene.
A credible multi-crop container business is therefore not "one pod that grows everything" but a standardised shell reconfigured by recipe, with crop classes grouped by compatible regimes and a central substrate or nursery line feeding them.
8. Sanitation, Sterilisation and Biosecurity
A sealed pod is a defensible perimeter, and the defensible perimeter is exactly why failures inside it are so expensive: there is no natural-enemy community, and a single aphid or thrips introduction into a warm, humid, pesticide-restricted volume multiplies unchecked.
Practical controls: a double-door airlock or gowning vestibule at personnel entry; filtered intake air; a quarantine bench with a rule that no incoming seedling enters the finishing room unobserved; documented seed and substrate sourcing, because many pathogen introductions arrive on the seed coat or in contaminated media; sticky traps and routine scouting as a data stream, not a formality; and tool, crate and hose hygiene between rooms, since the vector is usually a hand or a cart.
Surface sanitation in a wet, electrical enclosure is a design problem: cleanable surfaces, IP-rated fittings, drains that do not trap slurry under rack feet, and a wash-down protocol that does not damage the very components the room depends on. Where biological control agents are used, the pod must be treated as a release enclosure — beneficials have no refuge from a mis-timed HVAC cycle or a broad-spectrum cleaning residue.
9. Control Layer, Sensing and Data
A competent container runs cascaded loops on air temperature, humidity, solution temperature, pH, EC, dissolved oxygen and CO₂, logging every channel with alarms on deviation. The differentiators are:
- Redundant sensing at both ends of the room and at two heights. The crop only experiences canopy level, and canopy level differs from the reading beside the controller.
- VPD computed and controlled, not temperature and humidity independently.
- Documented fail-safe states. A dosing pump stuck open overshoots EC within minutes; a solenoid stuck open floods; a humidifier left on a bad reading wets walls and triggers a mould event. Ask what each actuator does on loss of signal and loss of power.
- Recipe management with per-batch environmental logging, so that a specific harvest lot can be reconstructed for root-cause analysis and for traceability.
- Remote operability. Single-phone supervision of several pods collapses the labour line, which is the dominant recurring cost in fresh produce; this is a genuine productivity feature, not a convenience.
- Power resilience. A short outage is survivable in deep-water culture and can be fatal in NFT or aeroponics within an hour in a warm climate. Automatic restart, phase-loss protection and a UPS or generator path for pumps and controllers are structural, not optional, in those architectures.
10. Utilities, Siting and the Unbudgeted Items
Containers get delivered to sites that cannot feed them. The items most frequently discovered late are electrical service capacity and phase (a lighting-dense pod is an industrial load), water supply quality and testing, condensate and nutrient-discharge disposal permissions, refrigerant handling and certification marks for the destination jurisdiction, crane or dock access for delivery and set, noise limits near residential boundaries, and local fire-code treatment of high-density electrical loads inside an occupied enclosure. Treating the unit as "equipment" rather than "a building" shortens the permit path in many jurisdictions, but it does not exempt the site from service, discharge and refrigerant rules.
11. Reliability, Redundancy and Fleet Logic
One pod has no redundancy: a compressor failure, a dosing error, a contamination event or a labour gap stalls the entire pipeline. Commercial deployments therefore use N+1 modules on staggered cycles, so a room coming off harvest is available for clean-down while another reloads. The stagger is the actual product; the container is the component. Service dependency belongs in the same calculation — spare-part lead times for lamps, drivers, pumps and compressors, and remote-diagnostic capability, because a four-week driver lead time is four weeks of lost crop.
12. Unit Economics and the Metrics Worth Using
The container is one line in the cost stack. Capital includes module and envelope, lighting (often the largest single component and the fastest to become obsolete), HVAC with genuine latent capacity, racking, irrigation and dosing, reservoir and chilling, seedling capability or a purchase agreement, and wash/precool/pack — plus the unbudgeted utility items above. Operating cost is dominated by electricity (lighting and dehumidification), then labour, which for leafy and fruiting crops remains the largest recurring line because sowing, tending, harvesting and packing are still hand work, then nutrients, seed, substrate, chemicals, and losses.
Useful metrics, rather than marketing numbers: saleable Grade-A kg per m² of canopy per week, grams of saleable product per kWh, litres of freshwater per kg, cycle time from sow to cut including fallow and clean-down, and first-pass grade yield. Biological productivity per square metre is easy to claim; grade-adjusted throughput per unit of electricity and per unit of labour is what determines survival. A resource ratio — "90% less water," "five times the productivity per footprint" — can be excellent while the business loses money, because the ratio is not the margin.
13. Observed Failure Modes
- HVAC sized on cooling capacity, not dehumidification: temperature holds, humidity climbs, condensation forms, mould follows.
- Single-point sensing while the far end of the room runs a different climate, producing two grades from one batch.
- Low-VPD operation to "protect humidity," producing tip burn and structurally weak leaves that collapse in the bag.
- Fixture thermal mismanagement causing lumen depreciation and spectral drift, later misattributed to seed or nutrients.
- Nozzle and emitter fouling in NFT and aeroponic systems with no redundancy and no visible alarm — a crop lost in an afternoon.
- Reservoir temperature creep driving dissolved oxygen down and Pythium up, typically in summer, typically blamed on the seed supplier.
- Ion accumulation in a closed loop with neither exchange nor removal.
- Light leakage bolting long-day crops.
- Condensate dripping onto the canopy, causing both disease and cosmetic grade loss.
- Missing workflow design: a pod that grows well but has no room for a sowing bench, a crate, a wash station, a cold box or a person to turn around loses more to handling than to horticulture.
- Cycle-time optimism that omits clean-down, drying, fallow and labour reality.
14. Buyer's Due-Diligence Checklist
- Request the latent-load calculation with assumed canopy density, fixture power per m² and design outdoor condition, plus the resulting dehumidification capacity in litres per day.
- Ask for measured PPFD maps and DLI at canopy level, not figures derived from fixture datasheets, with uniformity across the widest rack.
- Confirm fixture and driver IP rating, mounting location and warranty for a high-humidity environment.
- Verify multi-position, multi-height canopy-level sensing and how VPD is computed and alarmed.
- Establish fail-safe states for every actuator on signal and power loss, with pump/controller backup.
- Insist on disinfection dose validation for the nutrient loop, with UVT assumptions stated.
- Check reservoir volume, chilling and solution-exchange policy, including where spent solution goes and whether discharge is permitted on site.
- Inspect for cleanability: drains, rack feet, cable penetrations, light fittings, and whether surfaces can be washed without damaging electrical components.
- Obtain electrical, refrigerant and machinery certifications for the destination jurisdiction, in writing, with model numbers.
- Test transition behaviour: how fast the room moves between regimes — a finishing setpoint to a hardening setpoint, or a colonisation phase to a pinning trigger for fungal crops.
- Quantify service dependency: spare-part lead times and remote diagnostics.
- Run the model on grade-adjusted kg per m² per week and grams per kWh, with an explicit loss allowance.
- Confirm the site can supply power, water, drainage and access before the unit ships.
- Visit a unit at least six months into production, and look at the grading table rather than the canopy.
15. Direction of Travel
The category is moving from boxes toward process systems. Expect continued growth in dynamic spectral programming — far-red and UV protocols used to shape harvest index, flavour compounds, colour and shelf life rather than to maximise photon count; in model-predictive control that treats temperature, VPD and CO₂ as coupled variables and optimises against an energy price signal by shifting light and load within the day; in closed-loop nutrient management with partial ion recovery and validated disinfection, driven as much by discharge regulation as by water cost; in machine-vision phenotyping that estimates leaf area, biomass and defect incidence per tray and feeds it back into the climate recipe; and in robotic sowing, transplanting, harvesting and packing that attacks the labour line, which is where the cost actually sits. On the supply side, the market is consolidating around vendors who can document food-safety design, provide verified load sizing, and support a fleet rather than a single unit.
Structurally, the configuration that scales is unlikely to be the heroic single container. It is centralised propagation, distributed finishing, standardised shells reconfigured by recipe, and a data layer that makes every room interchangeable — because that architecture converts the two hardest problems in this business, contamination control and labour scheduling, from craft into process.
The framing that applies to any decision in this space is the same one that applies to its fungal equivalent, with the emphasis shifted: a well-engineered container solves the environment problem, and in photosynthetic crops the environment problem is larger and more expensive than it looks, because light is the input and heat and water are its unavoidable by-products. It does not solve seedling quality, nutrient discipline, grade-out, labour or market access. Those remain the business — and they are the reasons the format succeeds in a desert, a polar station, an ocean voyage or a land-scarce city, and fails, quietly, in a field.
On evidence and boundaries: this article describes established engineering practice in controlled-environment plant production. The numeric ranges cited — PPFD and DLI bands, fixture efficacy, EC and VPD windows, CO₂ enrichment levels, dehumidification sizing logic — are typical engineering bands rather than fixed specifications, and correct values depend on crop class, genotype, site climate, energy price and target grade. Food-safety, electrical, refrigerant, discharge and produce-safety obligations differ by country, state and destination market and are amended over time; confirm against the current text of the applicable authority before committing to a build, an export or any compliance claim. No specific vendor, product or market-size figure is asserted here.